03 / Case Study
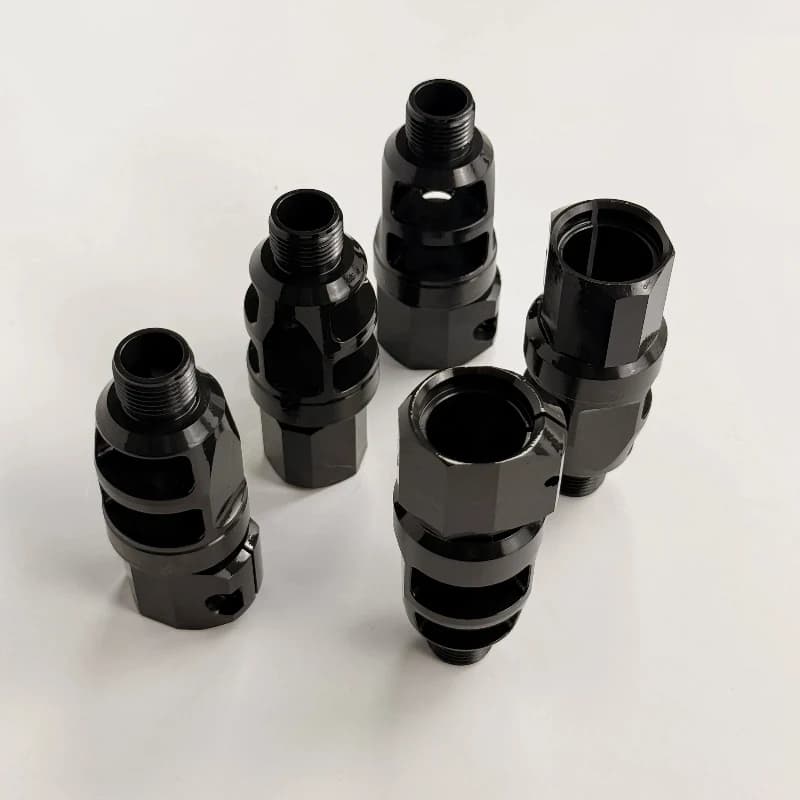
A 4140 steel connector combining turning, milling and EDM before a project-specified QPQ treatment and final inspection.
Engineering Record
The connector brought internal and external threads, side windows and hexagonal geometry together on one compact component. It therefore required several manufacturing methods and a sequence that considered both access to narrow corners and the dimensional effect of the specified post-machining treatment.
Each operation depended on a stable reference from the previous one. The process plan therefore had to retain the relationship between the turned body, milled openings and confined EDM features through finishing and final inspection.
The rotational body and internal and external threads were produced first. Milling created the side windows and hexagonal form, while EDM was reserved for confined internal corners that were not suited to conventional cutting access.
Machining allowance was planned before the project-specific QPQ treatment to account for possible dimensional movement. Final dimensional inspection covered the threads, openings and external geometry after the complete process route.
The recorded checks confirmed the required thread, window and external-form features, and the finished fittings were accepted for equipment assembly. This case documents a customer-specified route; it does not establish QPQ as a standard catalog finish for every project.
Related Capabilities
Project Review
Upload your drawings and share the material, process and finishing requirements that matter to your project.
Upload Drawings & Request a Quote